Modular Water Treatment Plant Upgrade
Client – Scottish Water
A modular ceramic membrane upgrade for residents & businesses in Shetland. Increasing water capacity & quality.
The Challenge
Eela Water Treatment Works was built in 1978 near Ollaberry in Shetland. It supplies up to 4.3 megalitres of drinking water per day (Ml/d) to approximately 5,400 people and the Sullom Voe Oil Terminal. The site had a long history of microbiological and discolouration compliance challenges, driven by seasonal peaks in raw water manganese affecting water quality at the tap.
Scottish Water commissioned a major upgrade to resolve 29 residual risks identified in the Drinking Water Safety Plan. The aim was to improve water quality and strengthen long-term resilience for the local community and industrial users.
We were appointed as principal designer and principal contractor, delivering civil engineering, process engineering, MEICA, filtration, chemical dosing, clear water storage, and the commissioning of a new 5.7 Ml/d ceramic membrane treatment facility.
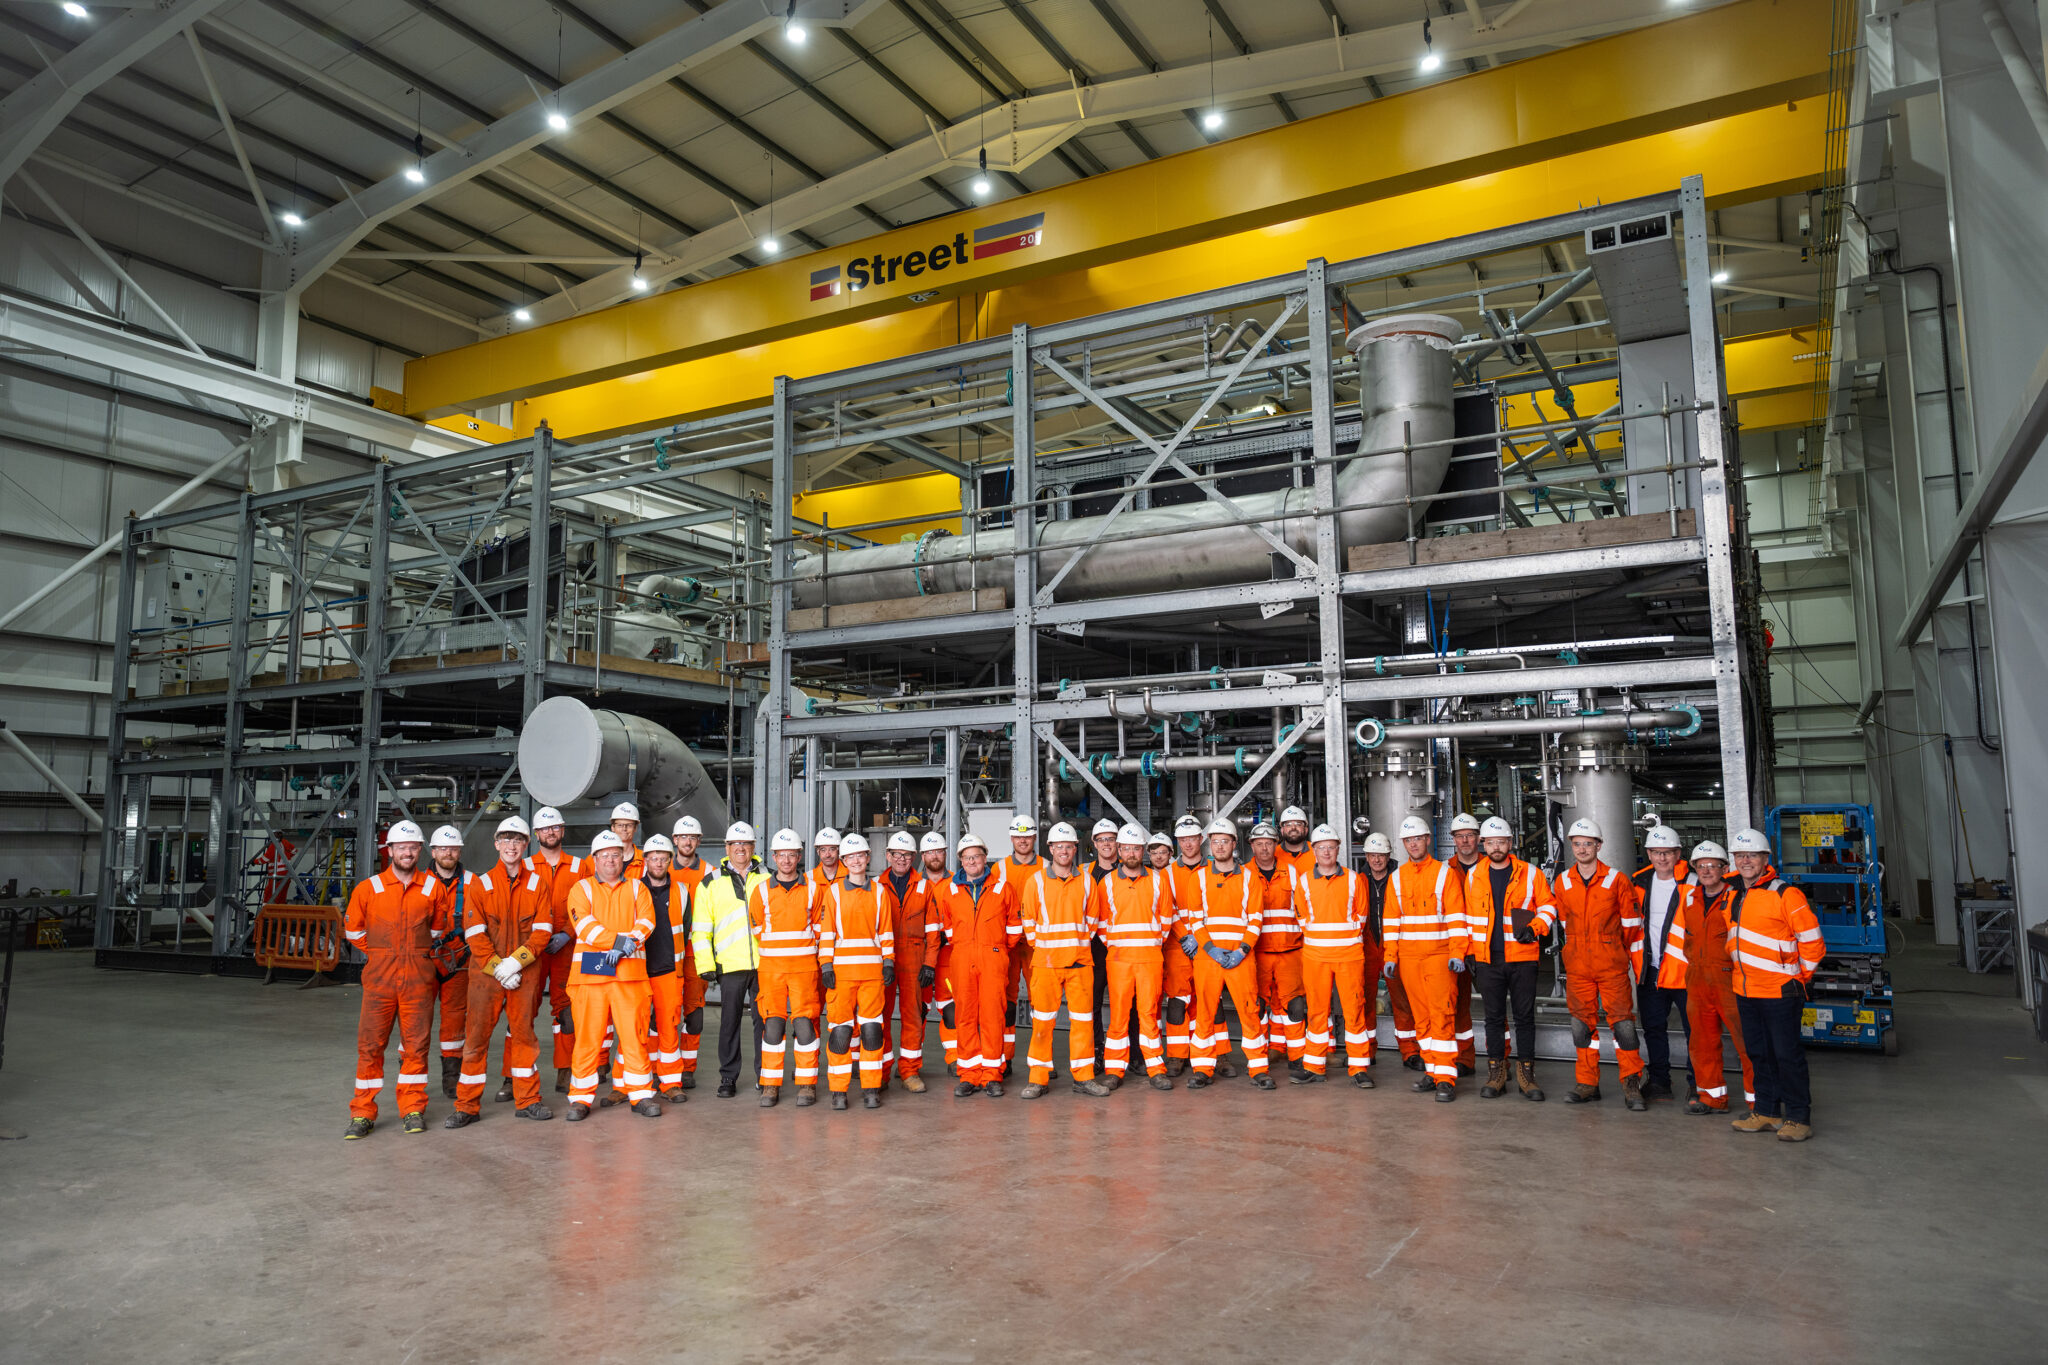
Production team delivering Eela WTW upgrade at RSE state-of-the-art fabrication facility in Muir of Ord.

Senior co-ordinators and apprentices working on the fabrication of the modular ceramic membrane plant for Eela WTW.

Assembly of 42 no factory-built TTUs allows for quality and programme savings.

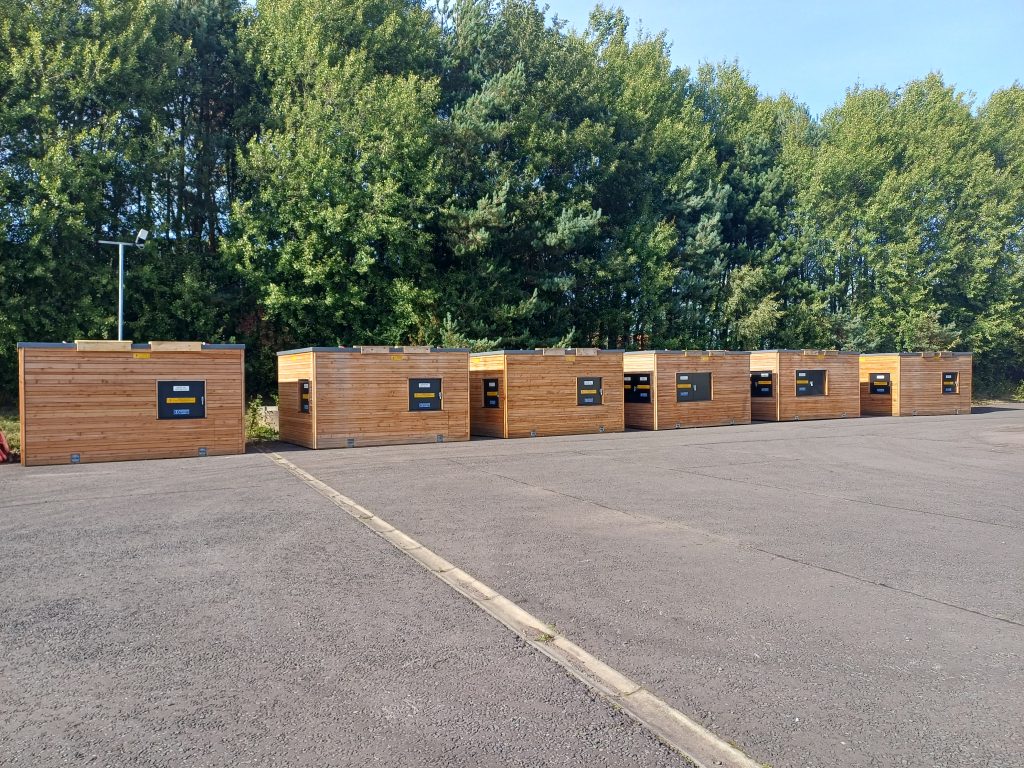
Eela WTW TTUs fabricated in modules before disassembly and transportation to site.

Eela WTW TTUs fabricated in modules before disassembly and transportation to site.
The Solution
Our solution centred on our modular CeraMac® ceramic membrane system, alongside other modular water treatment products from our range. Putting our Design for Manufacture and Assembly (DfMA) philosophy into practice, we built 42 Transportable Treatment Units (TTUs®) at our Muir of Ord facility in the Scottish Highlands to house the required technology, before transporting them by sea and road to the remote Shetland site. Off-site fabrication allowed testing and commissioning of the systems we designed under controlled factory conditions.
Our delivery team worked in close partnership with Scottish Water, heavy-lift and out-of-gauge cargo specialists and logistics partner Malin Group to ensure safe delivery. The first modules arrived on site in September 2025, with commissioning underway from January 2026 and water into supply due in March 2027.
To ensure every phase of delivery was as efficient as possible, our Business Information Modelling (BIM) team developed a 4D digital rehearsal. The team produced detailed 4D animations of the construction and installation sequence for the plant upgrade, enabling stakeholders to visualise the complete project delivery. This approach improves coordination across project teams, helping to identify potential issues early and providing a shared reference point for data-driven planning and decision-making.

“This project represents one of the most remote and logistically complex modular water treatment deployments in the UK, delivered at an unprecedented pace. Our modular approach allows for parallel construction, reduces programme risk and significantly cuts carbon.”
Duncan Gillies, Delivery Manager, RSE Treatment Solutions.


Eela WTW TTUs leaving Muir of Ord fabrication facility for transportation.

Eela WTW modules arrived at the Port of Cromarty Firth

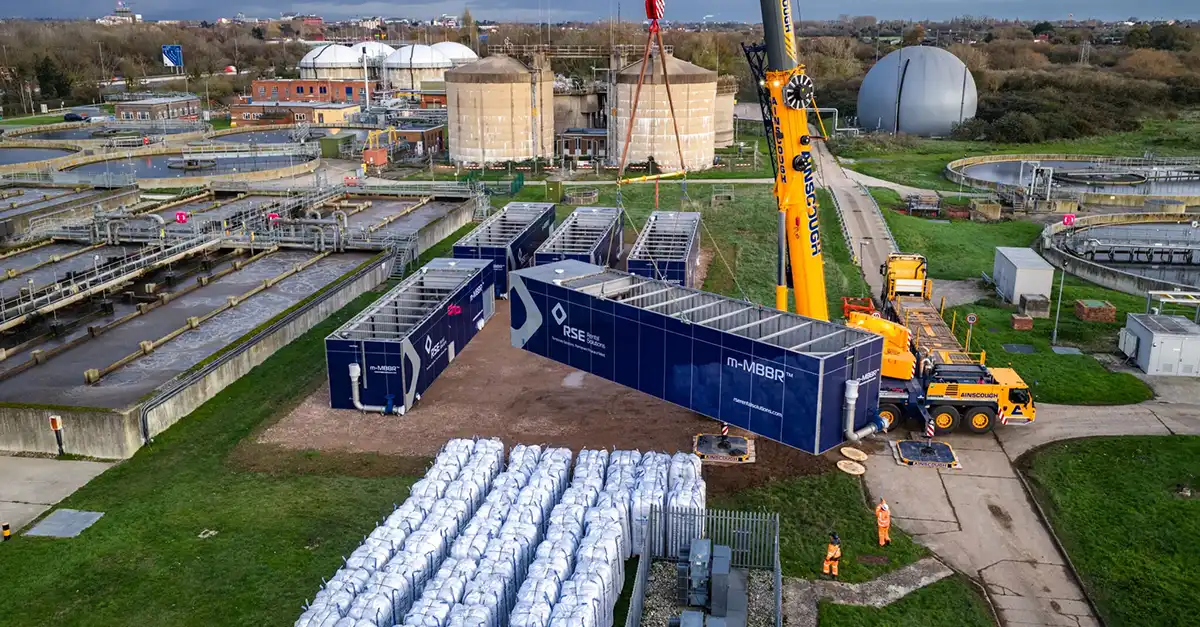
Loading of modular TTU suite for delivery to Eela WTW.

Loading of modular TTU suite for delivery to Eela WTW.

Transportation of modules to Shetland by marine logistics partner Malin Group.

Transportation of modules to Shetland by marine logistics partner Malin Group.
The Outcome
The upgraded works now include a multi-stage treatment process — pre-filtration, chemical dosing, coagulation, ceramic membrane filtration, limestone contactor treatment, and electrochlorination — supported by more than 70 SCADA-integrated sampling points for real-time monitoring and automated diversion of non-compliant water.
The modular units also achieved a 17% reduction in embodied carbon through low-carbon steel and bolted (rather than welded) construction.
The project earned RSE, in conjunction with Scottish Water, a finalist place at the Water Industry Awards 2026 in the Drinking Water Initiative of the Year.
“Our mission is to redefine how water treatment infrastructure is delivered. Through modular design, digital integration, and sustainable materials, RSE is setting new standards for quality, safety, and environmental responsibility.”
Michael Agolini, Head of Product Delivery, RSE Treatment Solutions

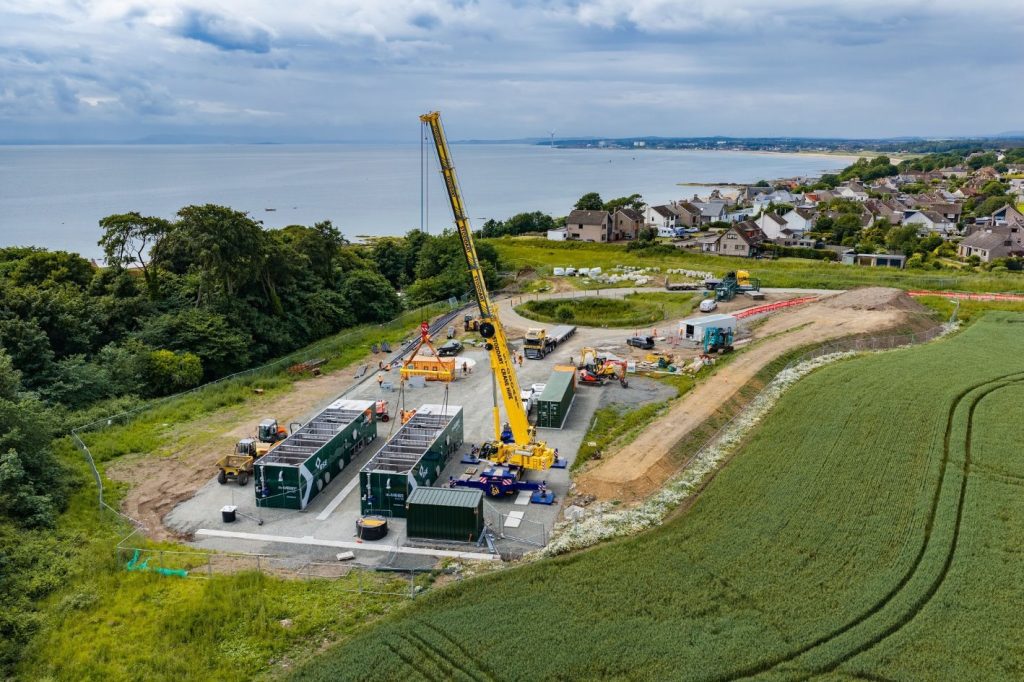
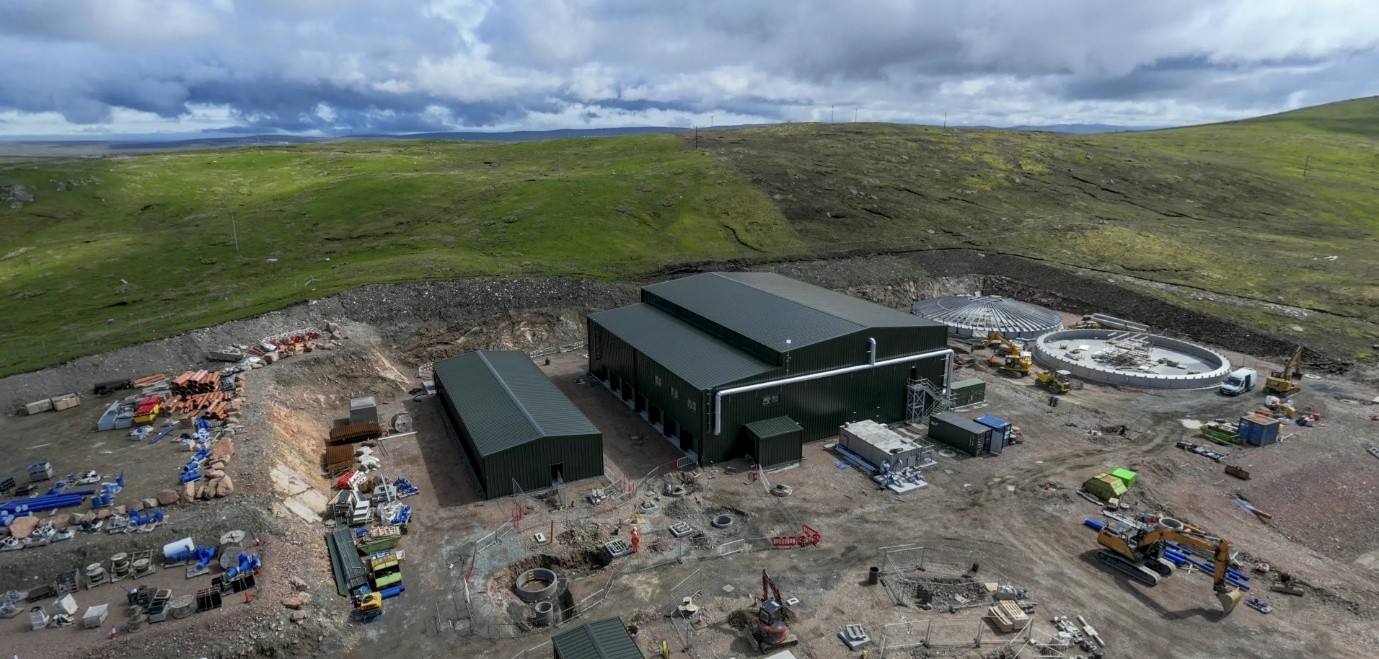
Construction works and assembly of first modular unit at Eela WTW on Shetland – August 2025.

Progressing site works at Eela WTW as Transportable Treatment Unit (TTU) modules arrive for installation – September 2025.

Progressing site works at Eela WTW as Transportable Treatment Unit (TTU) modules arrive for installation – October 2025.

Modular treatment units fully installed and clad forming the completed Eela WTW building – November 2025.


Want to Know More?
To find out more about how our modular approach speeds up delivery, reduces embodied carbon and supports the secure and sustainable growth of water infrastructure, click on the button below and please fill in the form. We’ll get back to you shortly.